
How do I measure products and boxes for custom box insert cavities?
Short answer: Measure the inside Length × Width × Depth of your outer box and subtract 1/16 to 1/8 inch for the insert tray perimeter. Then measure each item's length, width and thickness with calipers, leaving at least 0.5 inches of bridge spacing between wells on custom box inserts.
On this page
- How do I measure the inside of my outer box for an insert tray
- What are the exact clearance and pinch-fit tolerances by insert material
- How do I measure bottles, jars, tubes and tapered items accurately
- How do stepped cavity depths keep uneven products flush at the top
- Where should I place bridge walls and semicircular thumb notches
- Common mistakes
- FAQs
Request a custom quoteFree dieline & 3D mockup
Sizing a custom box insert requires two coordinated sets of measurements: the usable interior cavity of the outer box, and the three-dimensional profile of every product sitting inside the tray. Never size an insert from the outside dimensions of a box, especially on corrugated roll-end mailers where double-folded side walls consume up to 0.375 inches of internal width. The outer footprint of your insert tray should be 1/16 inch (0.0625 in) to 1/8 inch (0.125 in) smaller than the box's true inside length and width so the tray drops in smoothly without bowing the box walls. For the individual product cutouts, paperboard and corrugated inserts use a +1/32 inch slip-fit allowance so rigid board edges do not scrape labels, whereas closed-cell EVA and EPE foam inserts use a -1/32 to -1/16 inch pinch-fit interference so the foam hugs each bottle firmly.
How do I measure the inside of my outer box for an insert tray?
Always start by assembling a physical sample of your outer folding carton, corrugated mailer or rigid box and measuring the open interior floor from inside wall to inside wall. On a standard paperboard folding carton, the board thickness is thin enough that inside and outside dimensions differ by less than 1/16 inch. On an E-flute or B-flute roll-end tuck-front mailer box, however, the left and right side walls fold over twice to lock into the floor slots, and the front tuck flaps slide inside those double walls. That construction reduces usable inside width by 0.25 to 0.375 inches compared with the flat exterior width. Once you record the true inside Length × Width × Depth of the box, our design team sizes the outer perimeter of your custom die-cut box inserts 1/16 inch smaller on rigid boxes and 1/8 inch smaller on corrugated mailers. That small perimeter clearance lets your fulfillment team slide the tray to the bottom of the box in one motion without catching on glue seams or corner locks.
- Assemble the box completely: fold all side locks and dust flaps before measuring the interior floor.
- Measure inside Length (L): left-to-right distance between the inner faces of the side walls.
- Measure inside Width (W): front-to-back distance from the hinge wall to the inside of the front wall.
- Measure usable Depth (D): vertical distance from the box floor to the underside of the closed lid.
What are the exact clearance and pinch-fit tolerances by insert material?
Different insert materials behave very differently when a glass bottle, aluminum tin or electronic device is pressed into a die-cut well. Paperboard, fluted corrugated board and kraft honeycomb do not stretch elastically; if a cutout is even 1/32 inch narrower than a glass jar, the board edge will crease or scrape the paper label as you push the jar in. Closed-cell EVA and EPE foams, on the other hand, are designed to compress slightly and rebound against the product wall. Use the engineering reference table below to see how cavity cutouts, outer tray clearance and divider wall widths (called bridge widths) are calculated across all four decided CubitPack insert constructions.
| Insert material | Cavity cutout tolerance | Min bridge wall width | Tray-to-box outer clearance |
|---|---|---|---|
| Card insert (paperboard) | +1/32 in (+0.8 mm) slip fit | 0.375 in (9.5 mm) between cutouts | -1/16 in (-1.5 mm) under box L × W |
| Corrugated flute insert | +1/32 to +1/16 in slip fit | 0.5 in (12.7 mm) between cutouts | -1/8 in (-3.0 mm) under box L × W |
| EVA foam insert | -1/32 to -1/16 in pinch fit | 0.375 to 0.5 in between wells | 0 to -1/32 in snug fit in rigid box |
| EPE foam insert | -1/16 in (-1.5 mm) pinch fit | 0.5 to 0.75 in for shock absorption | -1/16 in under shipping box L × W |
| Honeycomb paper insert | Exact size to +1/32 in compression fit | 0.625 to 0.75 in hex-cell wall | -1/16 to -1/8 in under box L × W |
| Interlocking grid partitions | +1/16 in per cell for easy loading | Full cell wall between bottles | -1/8 in across assembled grid |
How do I measure bottles, jars, tubes and tapered items accurately?
Put away flexible cloth sewing tapes and use a digital caliper or rigid steel ruler to measure the physical product in three axes. If the product sits upright in the insert (like a candle tumbler inside a tall gift box), measure the base diameter, widest body diameter and total height. If the product lies flat on its back facing the customer (like a serum dropper bottle, mascara tube or perfume flacon inside a mailer or magnetic rigid box), measure the total length from cap tip to bottom base, the width across the shoulders, and the front-to-back thickness lying on the table. Watch out for three common geometry traps on cosmetic and beverage containers: flared pump collars, crimped squeeze-tube tails and tapered glass walls. A lotion pump collar is often 2 mm wider than the bottle neck, and a heat-sealed plastic cream tube flares wider at the top crimp than at the round cap. Always measure at every transition point along the item's silhouette so our CAD engineer can contour the cavity outline around pumps, droppers and shoulders.
Know your size? Compare pricing across up to 3 quantities.
Request a Quote →How do stepped cavity depths keep uneven products flush at the top?
In a multi-item starter kit or PR box, you rarely have three products of the exact same thickness. You might pair a 2.25 inch thick glass face cream jar with a 1.25 inch diameter serum dropper bottle and a 0.5 inch flat Gua Sha stone tool. If you cut all three cavities to a uniform 2.25 inch depth, the serum bottle and stone tool sink deep into dark holes where customers can barely see or reach them. To create a high-end retail stage, we engineer stepped cavity depths so the top face of every product aligns on the exact same horizontal plane just below the lid. Using the example above inside a 2.5 inch deep tray, the cream jar cavity is cut 2.0 inches deep, the serum bottle cavity is stepped to 1.0 inch deep, and the flat tool recess is routed 0.375 inches deep. On custom eva foam inserts and custom epe foam inserts, we achieve stepped depths by laminating die-cut foam layers of different thicknesses over a solid base layer; on custom cardboard inserts, we fold internal support legs to hold lighter items higher.
Where should I place bridge walls and semicircular thumb notches?
After sizing the individual cavities, you need enough structural wall material (called the bridge) between each cutout and around the outer border of the tray. Keep at least 0.5 inches of bridge width between adjacent wells and at least 0.5 to 0.75 inches around the outer perimeter next to the box walls. When shipping heavy glass jars, beverages or ceramics, widen the outer perimeter border to 0.75 or 1.0 inch so a corner drop on concrete cannot crush through the buffer zone. Finally, every snug foam or paperboard cavity that holds an item flush with the top deck needs two semicircular thumb notches (typically 0.625 to 0.75 inches in diameter) positioned on opposite sides of the product's balance point. Without thumb cutouts, customers have to dig their fingernails into the foam edge or turn the entire box upside down to shake the product loose.
- Inter-cavity bridge width: minimum 0.375 to 0.5 in for cosmetics; 0.5 to 0.75 in for heavy jars.
- Outer perimeter buffer: 0.5 in minimum for rigid boxes; 0.75 to 1.0 in for parcel shipping boxes.
- Thumb notch diameter: 0.625 to 0.75 in half-moon cutouts placed opposite each other.
- Neck-lock tabs: add folded retention wings over narrow dropper necks to stop vertical slide.
What are the most common box insert measurement mistakes?
Measuring errors almost always come from ignoring inner box wall folds or skipping thumb clearance on flush-mounted cavities. Avoid these five mistakes
- Using the outside dimensions of a corrugated mailer box as the insert tray size, which makes the insert 0.25 to 0.375 inches too wide to fit between the double side walls.
- Measuring only the round barrel of a squeeze tube and forgetting the wider flat crimp at the tail end.
- Cutting paperboard cavities with zero slip-fit clearance, causing the sharp cardstock edge to scuff matte bottle labels during packing.
- Placing two heavy glass jars only 0.125 inches apart, leaving a paper-thin bridge wall that buckles on the first parcel drop.
- Skipping semicircular finger notches on flush-mounted EVA foam wells so customers cannot lift out palettes or bottles.
Packaging for this

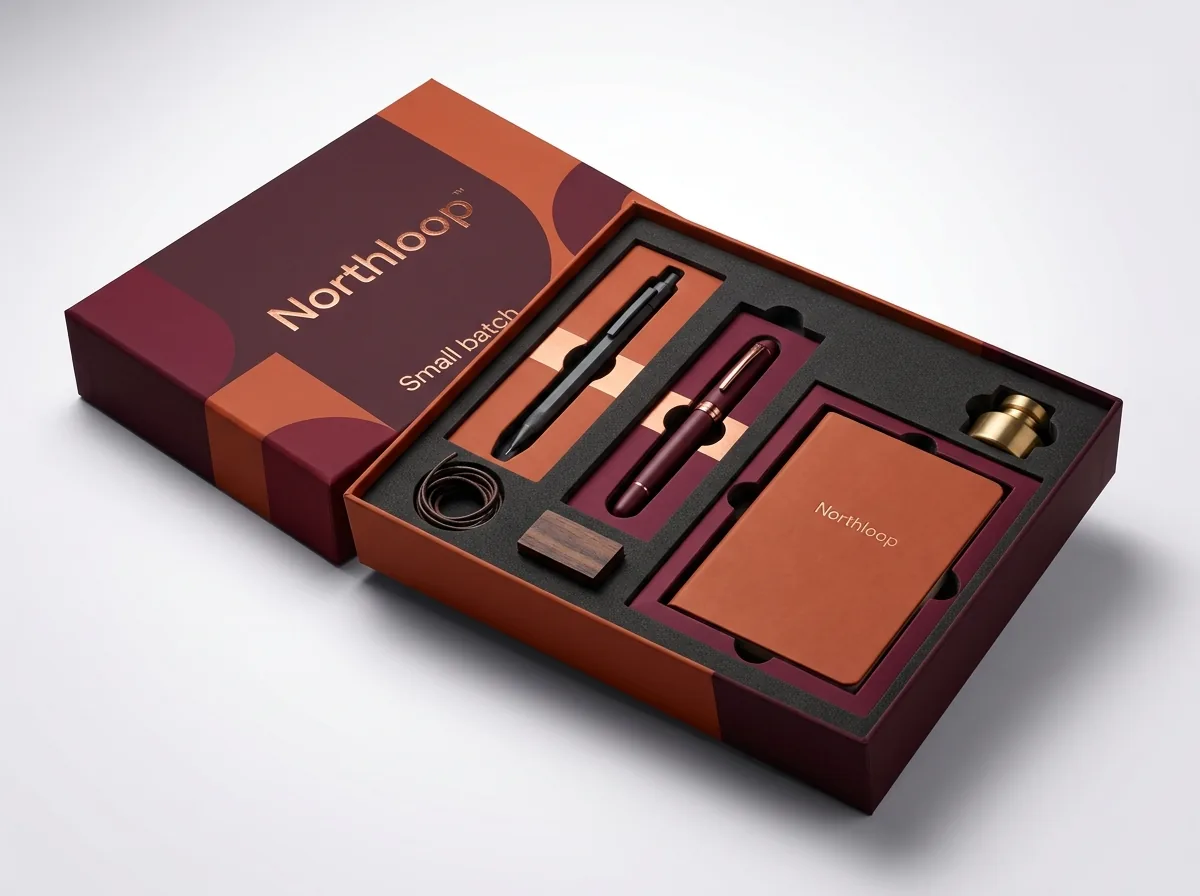
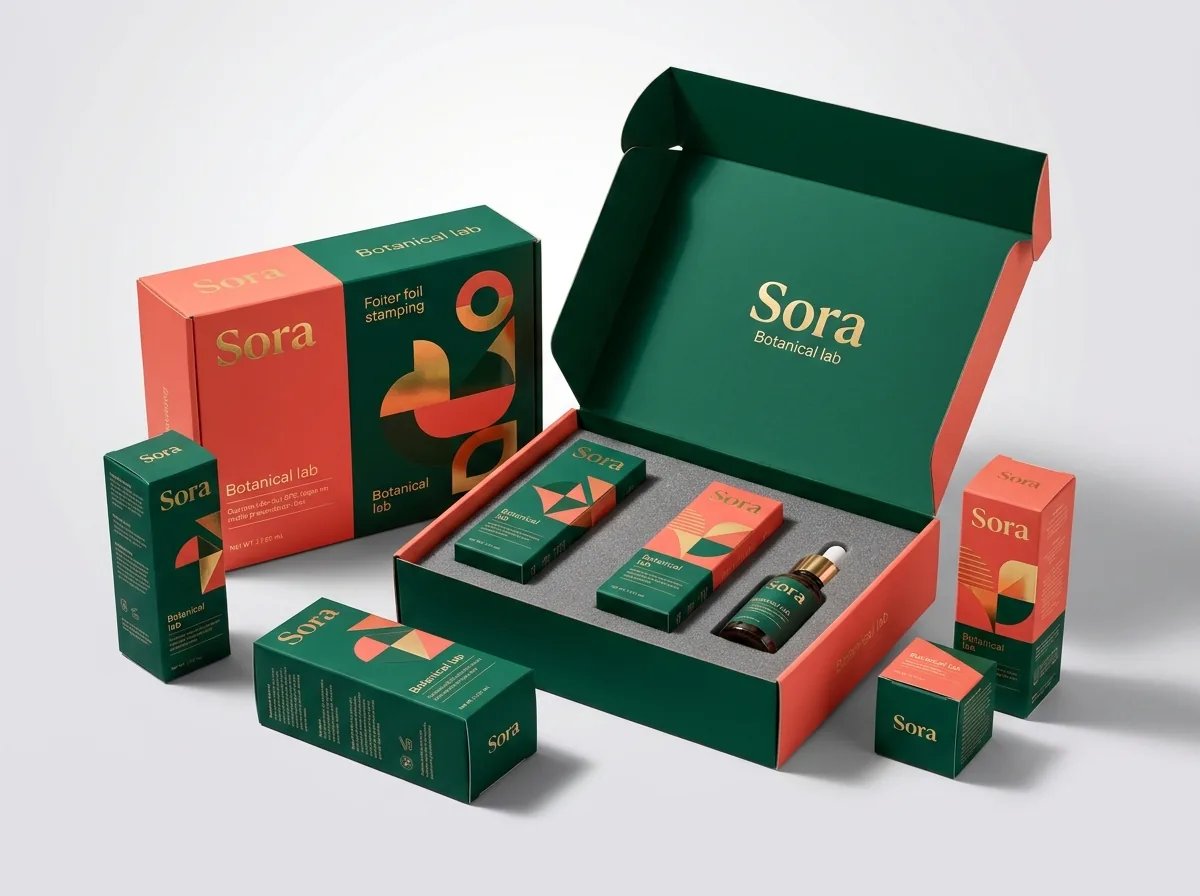
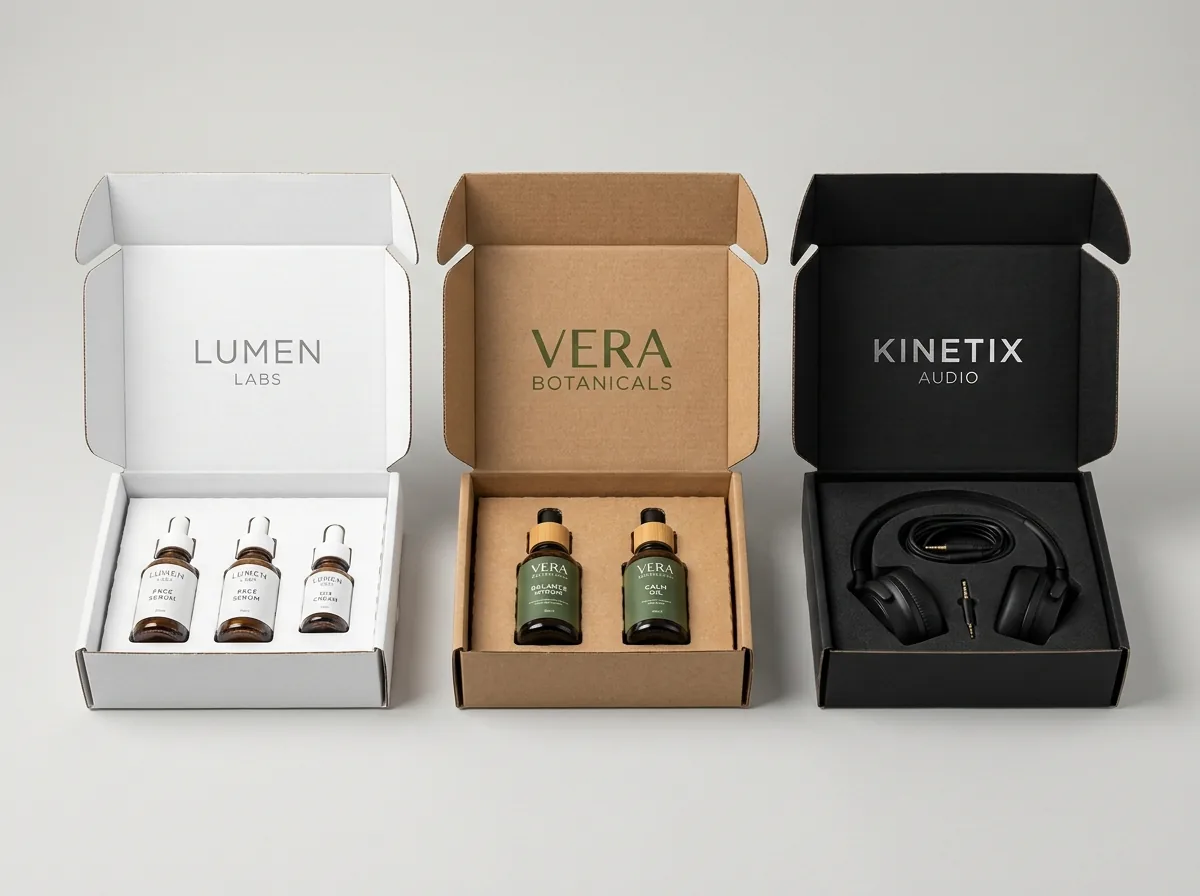
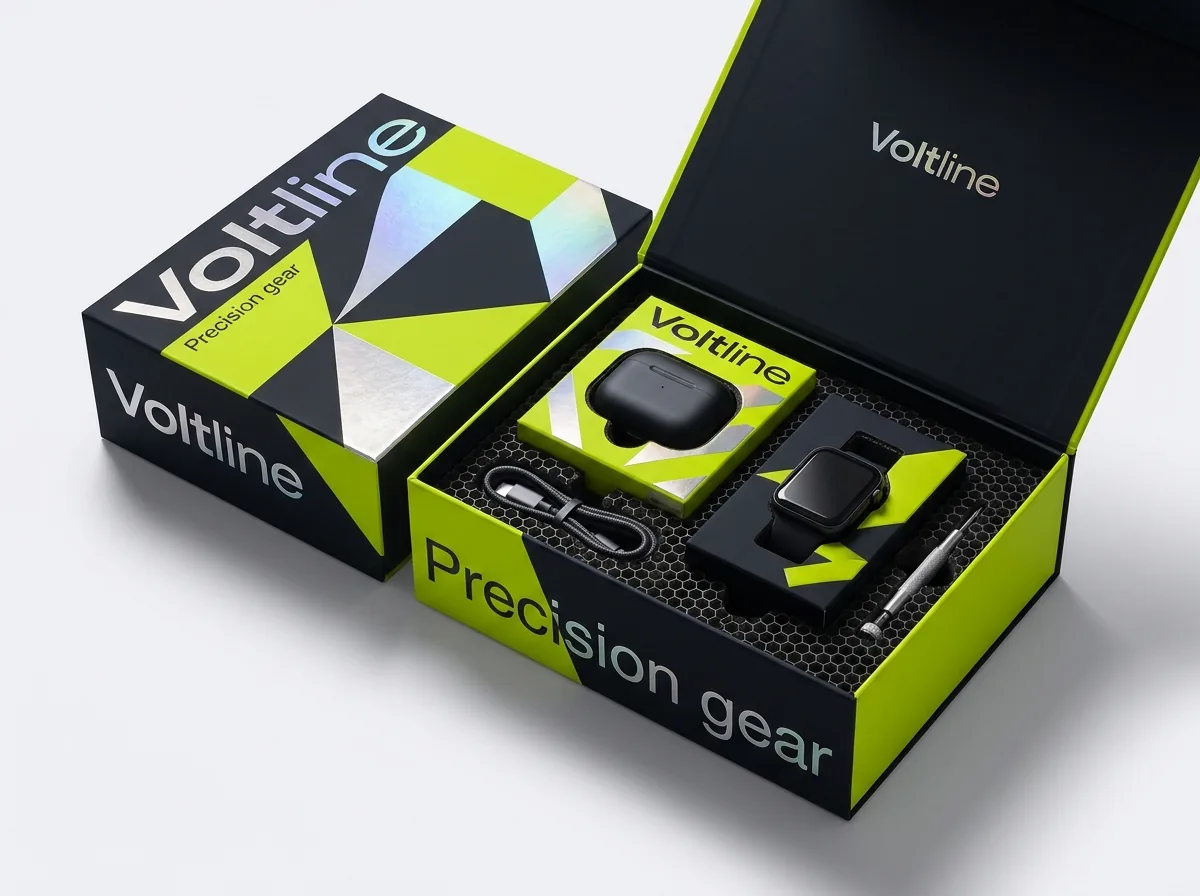
Ready to order box inserts? Compare up to 3 quantities with a free 3D mockup.
Request a Quote →Questions about box inserts
Should I measure my products in inches or millimeters for a custom insert?
You can enter outer tray dimensions in inches in the quote form and list individual product measurements in either inches (to the sixteenth of an inch) or millimeters in the notes. Digital calipers set to millimeters are especially helpful for small dropper necks and vials.
How much smaller than the box interior should a folded cardboard insert be?
A folded paperboard insert inside a folding carton should be about 1/16 inch (0.0625 in) smaller than the box's internal length and width. Inside a corrugated mailer box, make the insert 1/8 inch (0.125 in) smaller to clear flute tolerances.
What is pinch-fit interference on an EVA or EPE foam insert?
Pinch-fit interference means cutting the foam cavity 1/32 to 1/16 inch (0.8 to 1.5 mm) narrower than the rigid bottle or device. When the item is pressed into the well, the closed-cell foam walls compress slightly and grip the item so it cannot fall out.
How deep should a cavity be if my product sits flush with the top of the insert?
For a flush presentation where the product's top face sits level with the insert deck, make the cavity depth equal to the product's laying-flat thickness (plus a 1/16 inch base foam pad underneath so the item never touches the raw bottom of the box).
Can I mail you my physical bottles or devices so your engineers can measure them?
Yes. Once you request a quote, your dedicated account manager can give you the shipping address to send physical product samples. Our structural designers will measure every contour with digital calipers and test-fit your prototype before production.
Do I pay extra for structural engineering or multi-depth cavity dielines?
No. Structural design, custom dielines, digital proofs and 3D mockups are always free at CubitPack, and we never charge cutting die or printing plate fees regardless of how many cavities your insert holds.
Still have a question? Ask a packaging specialist.
Request a Quote →Request your box inserts quote
Tell us your size and quantities, and one dedicated account manager prepares pricing for each tier.
- Free design & AI-to-print studio + 3D mockup
- No die or plate charges · 4–5 day rush available
- Free shipping to all 50 states
- 10% off your first order
The clearance tolerances (+1/32 in slip fit for paperboard, -1/32 to -1/16 in pinch fit for closed-cell foam, and 0.375 to 0.75 in bridge widths) follow standard CAD die-cutting and ISTA parcel transit practices, verified by a CubitPack packaging specialist. Spot an error? Tell us and we will fix it.
Sources
What changed
- October 22, 2026: First published.
- October 22, 2026: Updated specifications, terminology, and verified source links.
More guides
New packaging guides by email
Sizes, materials and design tips. Unsubscribe anytime.